Manufacturing Facility
A state-of-the-art dairy plant, built for purity
Modern technology, separate in-house labs and hands-free, positive-pressure packing — so every Bristol product is safe, hygienic and consistent.
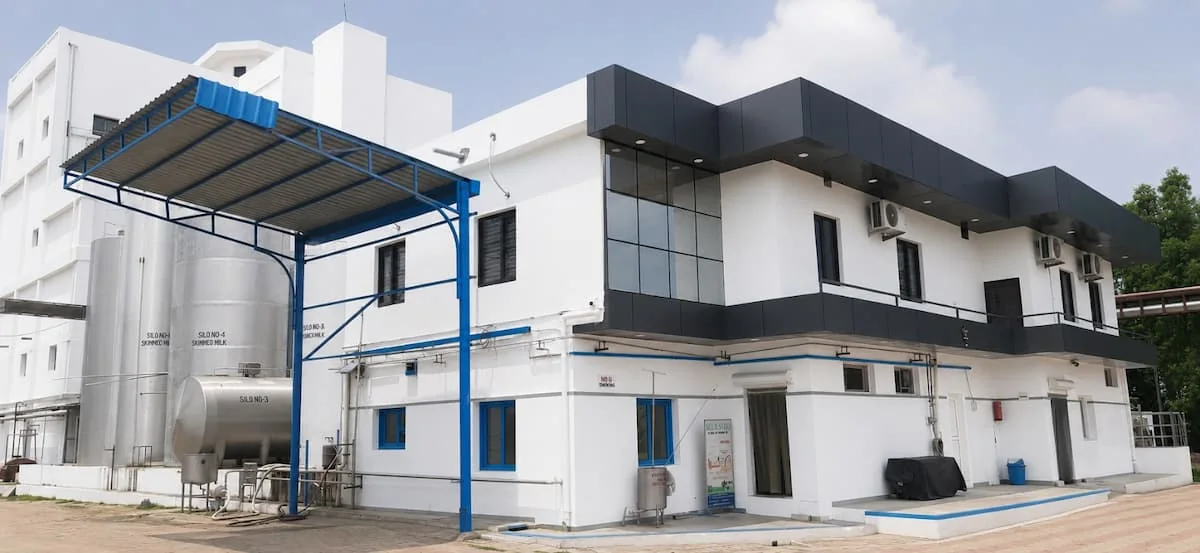
Plant Areas
From separation to packaging
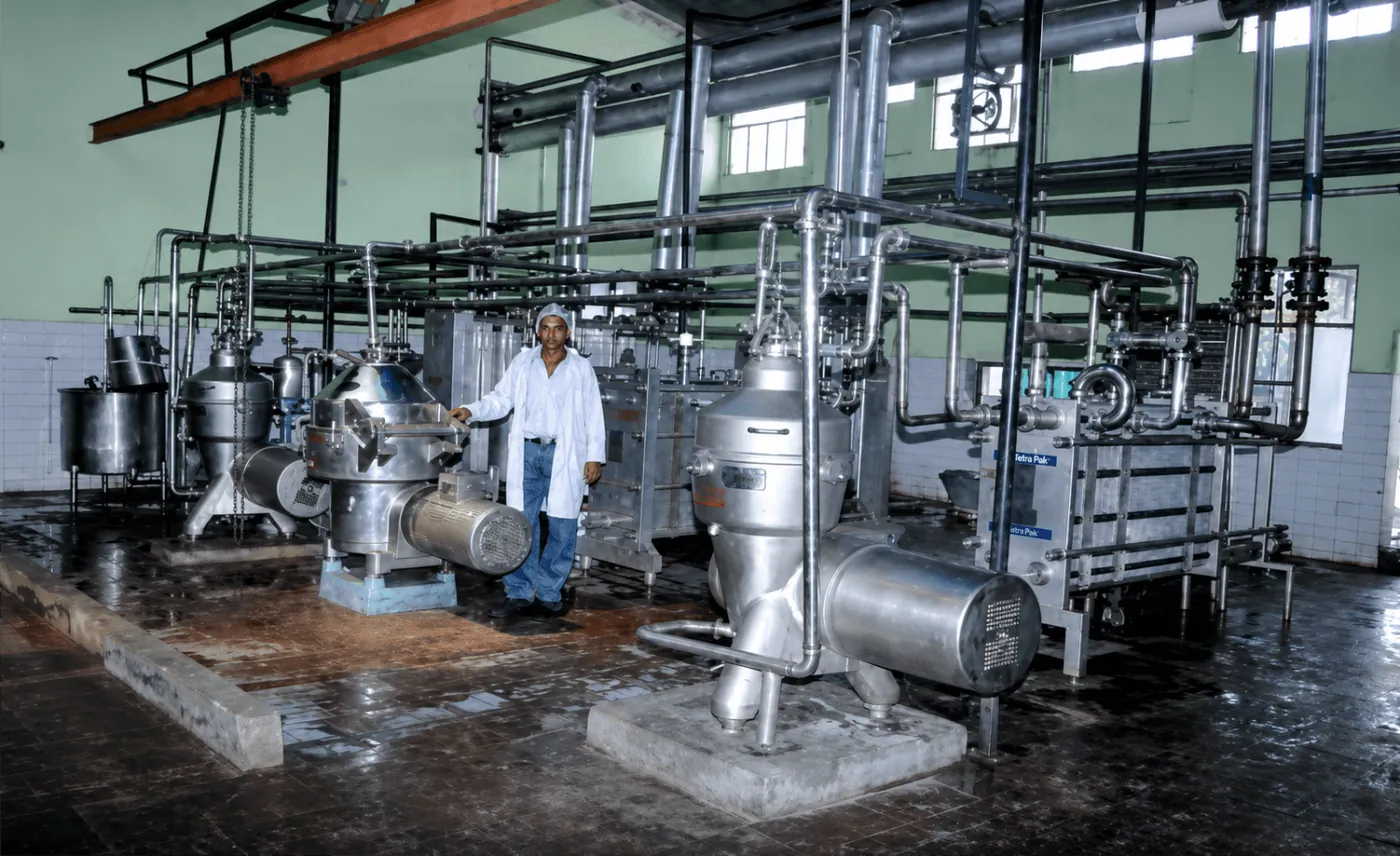
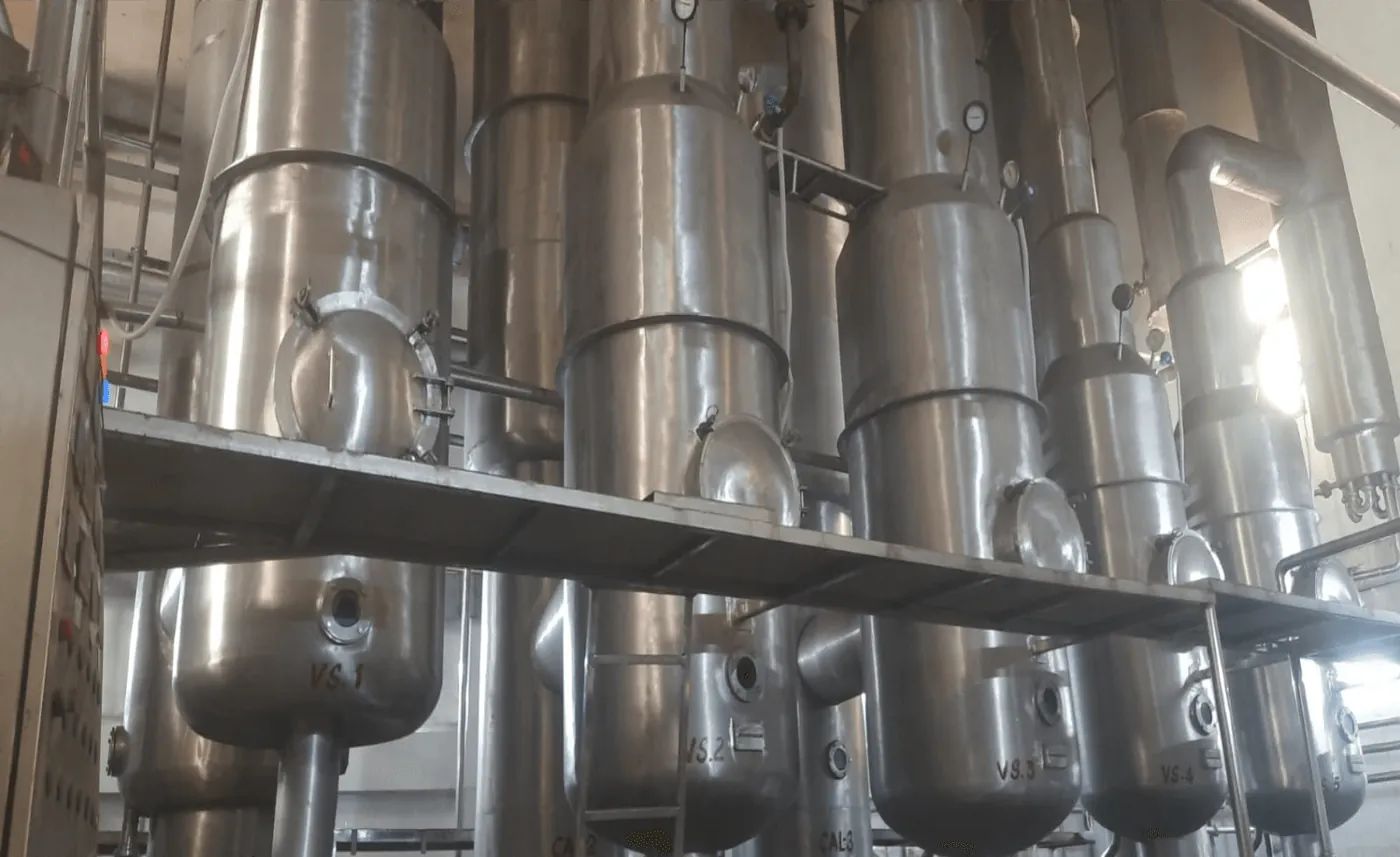
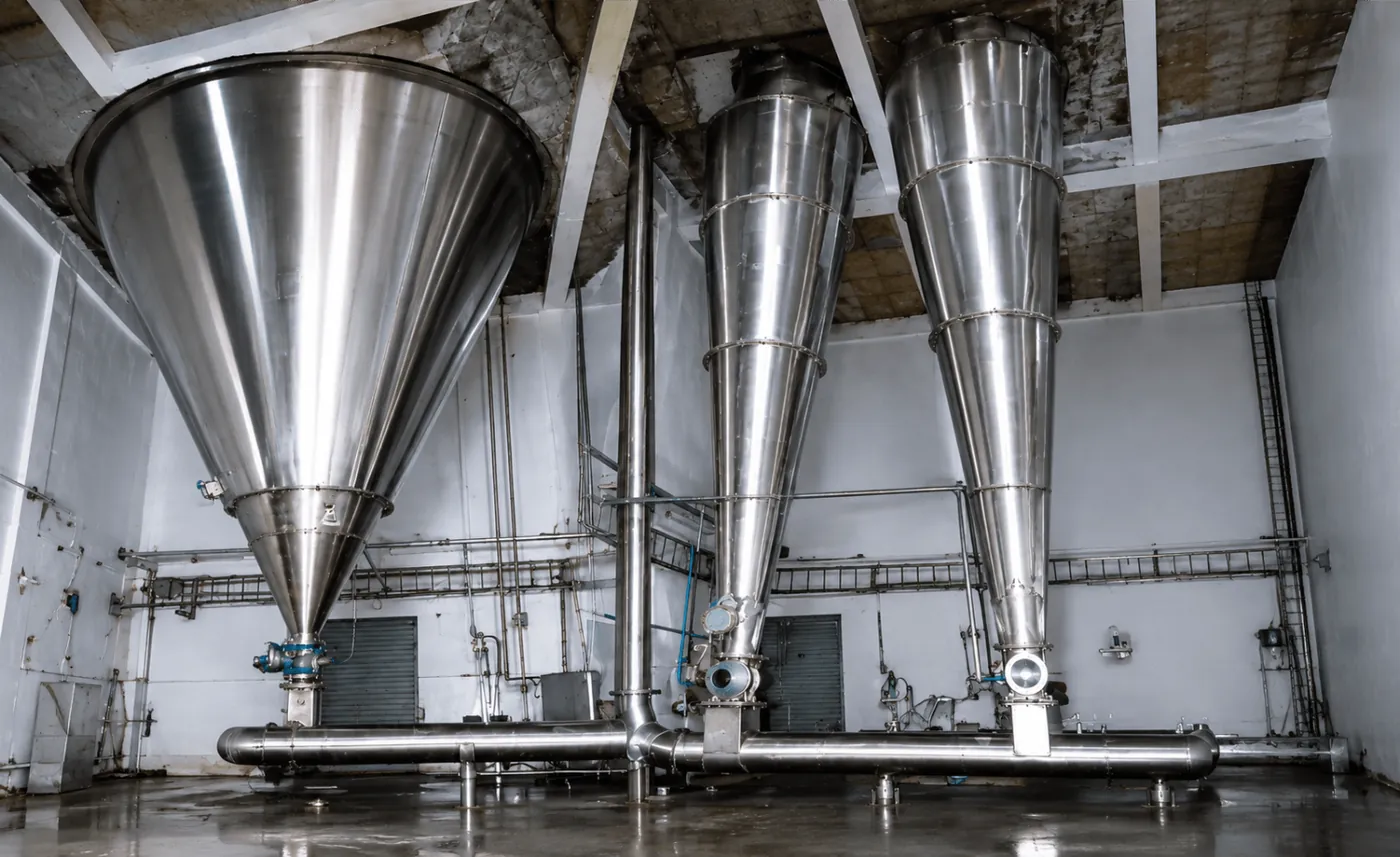
Technology
Latest equipment for maximum productivity
Butter Churner
Modern churning for consistent, high-quality butter.
Auto Butter Transfer System
Hands-free transfer of butter for superior hygiene.
Milk Separator (10 KL)
High-capacity separation for cream and skimmed milk.
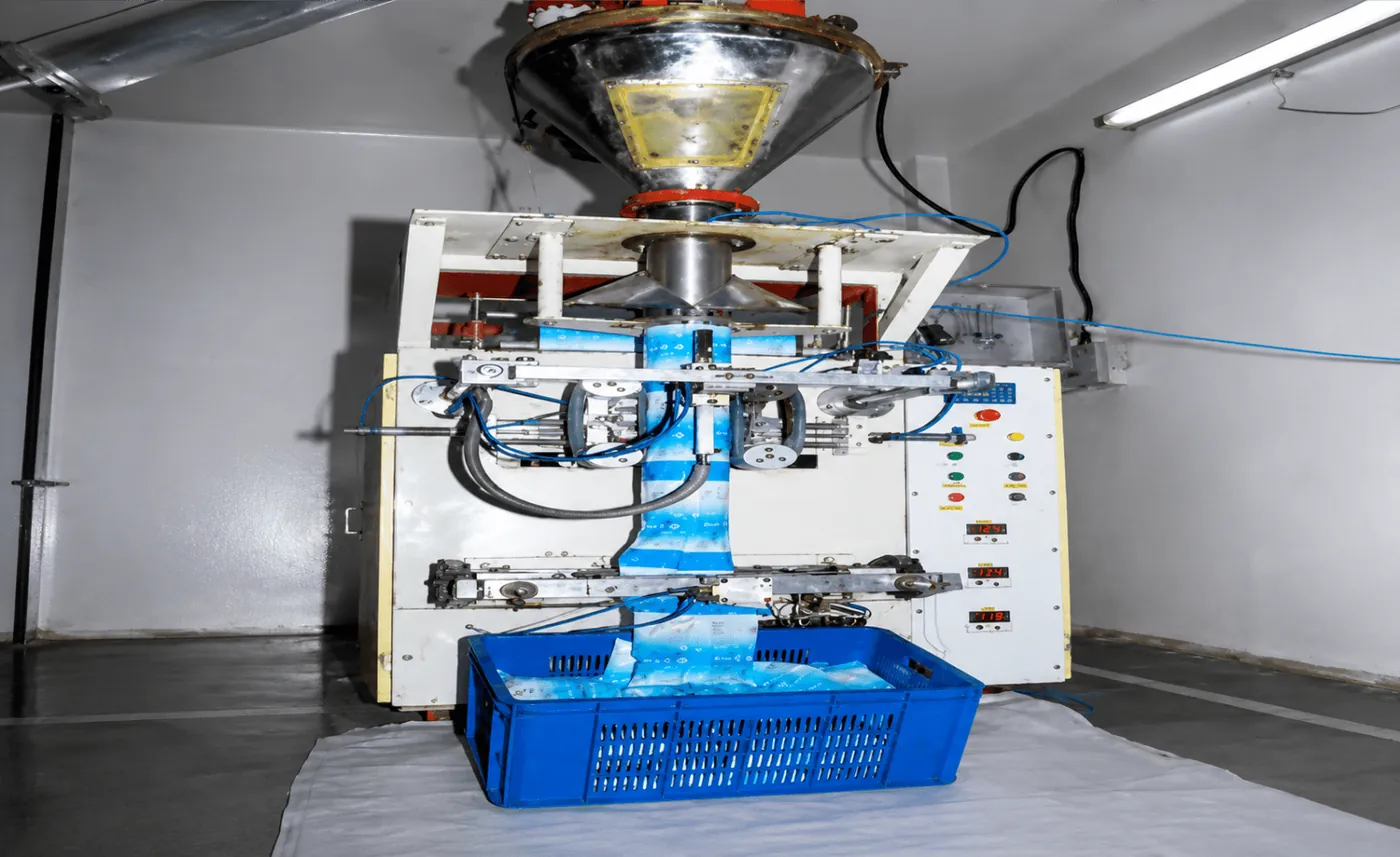
Hassia FFS Machine
Automated form-fill-seal packing for precise, sealed packs.
Blast Cold Rooms
Rapid chilling and cold storage to lock in freshness.
Positive-Pressure Packing
Hygienically controlled, hands-free packing environment.
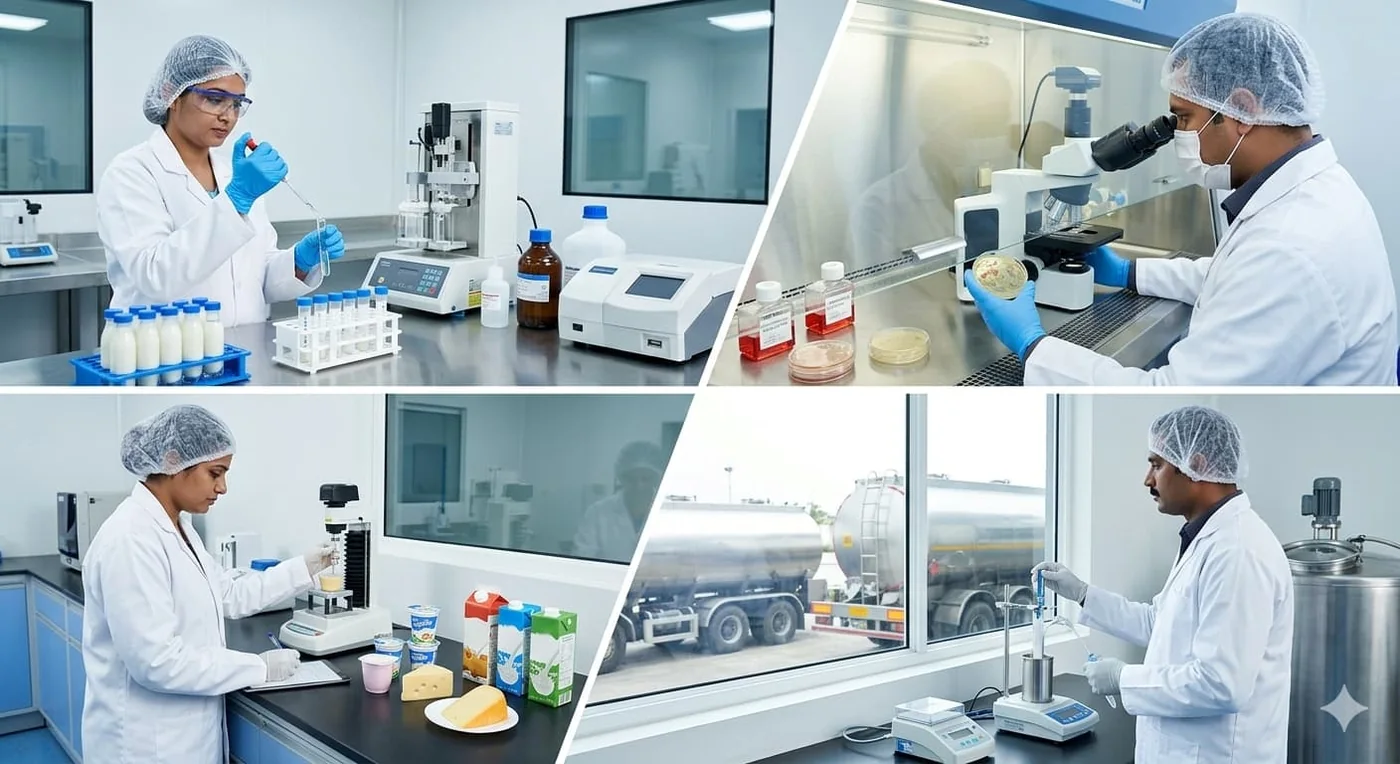
In-house Laboratories
Four labs. 27 quality checks.
Separate chemical, microbiological, product and raw-material labs test milk and products at every stage — from intake to dispatch.
- Chemical lab
- Microbiological lab
- Product lab
- Raw material lab
Installed Capacity
Installed capacity per day
| Product | Capacity / day |
|---|---|
| Milk processing | 2,50,000 L |
| Skimmed Milk Powder | 20 Tons |
| Whole Milk Powder | 15 Tons |
| Dairy Whitener / Creamer | 15 Tons |
| Butter | 20 Tons |
| Ghee | 15 Tons |
| Paneer | 10 Tons |
| Curd | 30 Tons |
 ISI · BISIS:13334 & IS:1165 milk powders BIS certified
Partner with Bristol
Looking for a reliable dairy ingredients partner?
Tell us your product, quantity and application — our team will share specifications, samples and pricing for bulk supply across India and exports.