Our Process
Six careful steps from village farm to your factory
A cold, clean and fully traceable chain — with stringent quality testing at every stage.
Step 1
Raw milk collected
Fresh milk collected from farmers twice a day, at village level.
Step 2
Tested & cooled to 4 °C
Milk is tested and chilled at our centres, then moved in insulated tankers to our plant.
Step 3
Stringent quality tests
Checks at intake ensure only superior-quality milk is used.
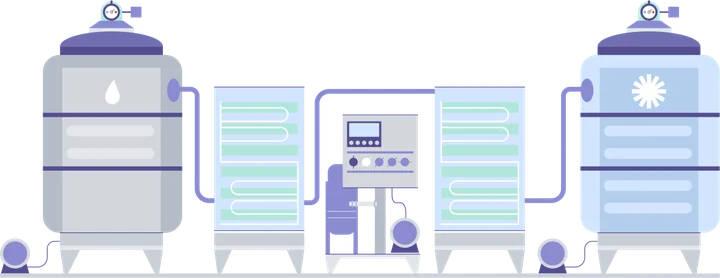
Step 4
Ultra-modern processing
Separation, evaporation and drying in our modern facility.
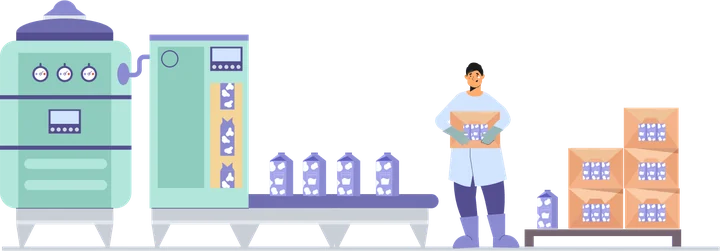
Step 5
Pasteurised & packed
Products are pasteurised, chilled and packed hands-free for hygiene.
Step 6
Delivered to you
Superior-quality products dispatched to distributors, retailers and food makers.
Cold chain at 4 °C
Milk is tested and cooled to 4 °C at village level for transport to our processing plant — preserving freshness from the very first step.
Hands-free & hygienic
Products are manufactured and packed under positive-pressure conditions in a hands-free environment.
Traceability
Know where every drop comes from
Our integrated model connects each stage — so milk can be traced from the village to the finished pack.
Farmer
Milk collected twice daily at village level
Chilling centre
6 MCCs with bulk milk coolers & analysers
Plant
Tested, processed & packed hands-free
You
Delivered across India and exported
Partner with Bristol
Looking for a reliable dairy ingredients partner?
Tell us your product, quantity and application — our team will share specifications, samples and pricing for bulk supply across India and exports.